Technical Specifications
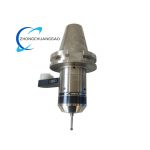
- Machine Taper Standard: BT50 Japanese industrial machine tool taper specification
- Hydraulic Chuck Clamping Diameter Range: 56mm nominal tool shank compatible diameter
- Overall Projection Length: 195mm from taper gauge line to chuck front face
- Maximum Safe Spindle Rotational Speed: 12,000 RPM balanced G2.5 grade dynamic balance
- Radial Runout Accuracy at 3x tool diameter: ≤ 0.001 mm precision tolerance
- Hydraulic Clamping Mechanism: Internal sealed oil pressure expansion sleeve
- Coolant Through Tool Compatibility: Internal central coolant bore passage
- Material Hardness: HRC 58–62 full body heat treatment hardness
Functional Features
- Uniform hydraulic radial clamping force eliminates uneven tool shank deformation during high-speed rotation
- Ultra-low radial runout maintains micron-level machining dimensional accuracy
- Central through-coolant channel delivers high-pressure cutting fluid directly to cutting edge
- Single-sided hydraulic actuation screw for rapid tool exchange without specialized clamping equipment
- High dynamic balance grade eliminates spindle vibration at maximum rated rotational speed
Structural Characteristics
- Integrated BT50 solid taper shank monolithic forged construction
- Mid-body hydraulic expansion sleeve encapsulated sealed oil chamber
- Front cylindrical chuck bore for straight tool shank insertion
- Side hydraulic pressure adjustment actuation screw for clamp/release operation
- Central axial through-hole for high-pressure coolant fluid transport
Material Composition
- Base body blank: Chromium-molybdenum alloy steel 42CrMo4
- Hydraulic expansion sleeve: High elastic alloy spring steel
- Sealing media: High temperature resistant nitrile hydraulic oil seals
- Internal hydraulic fluid: Anti-wear low-viscosity mineral hydraulic oil
- Surface coating: Black oxidation anti-corrosion wear resistant surface treatment
Working Principle
Insert straight shank cutting tool into front hydraulic chuck bore; rotate side actuation screw to compress internal sealed hydraulic oil chamber; incompressible hydraulic oil distributes uniform radial pressure to elastic expansion sleeve; sleeve contracts inward to fully grip tool shank across full contact surface; uniform clamping force eliminates point-contact runout error; reverse rotation of actuation screw releases hydraulic pressure, allowing free tool removal; central coolant bore routes machine spindle high-pressure cutting fluid through tool holder to cutting tool tip for continuous cooling and chip evacuation during material removal cycles.
Advantage Highlights
- Micron-grade radial runout tolerance delivers superior surface finish precision for mold and die machining
- Hydraulic clamping eliminates tool slippage under heavy interrupted milling cutting loads
- G2.5 factory pre-balanced construction prevents spindle chatter at high RPM machining
- Long 195mm projection length accommodates deep cavity mold machining without custom extension adapters
- Monolithic forged BT50 taper eliminates assembly tolerance stack-up error compared to modular tool holders
Applicable Industries
Precision mold & die CNC machining, automotive engine component milling, aerospace alloy part boring, medical implant precision machining, semiconductor mold fabrication
Installation Requirements
- Clean BT50 spindle taper surface and tool holder taper with lint-free solvent wipe prior mounting
- Mount holder fully seated into CNC machine BT50 spindle drawbar assembly
- Insert straight shank cutting tool fully into chuck bore before applying hydraulic clamping pressure
- Perform radial runout verification with dial indicator post tool exchange operation
- Calibrate machine spindle dynamic balance offset if utilizing custom heavy cutting tools
Usage Precautions
- Do not exceed maximum rated spindle speed 12,000 RPM during continuous machining cycles
- Remove all metal chip debris from chuck bore before inserting new cutting tool shanks
- Avoid over-tightening hydraulic actuation screw to prevent permanent expansion sleeve deformation
- Refill internal hydraulic oil chamber every 12 months of continuous production machining use
- Prevent direct collision between chuck front face and workpiece fixture during rapid machine axis movement
Reviews
There are no reviews yet.